o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
7 Tips for Buying PE Coloring Masterbatch?
Buying Pe Coloring Masterbatch is not simply a matter of choosing the brightest pellet. The decision affects color accuracy, processing stability, recycled-content performance, and finished-product cost. PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023, showing the enormous scale behind every small color decision. Grand View Research also estimates steady growth in the global masterbatch market, although market definitions differ between reports.
Small choices matter.
Tony Calverley, a longtime masterbatch industry consultant, offers a useful warning: “Color consistency begins with disciplined process control, not a lucky pigment choice.” This principle deserves attention when comparing pigment concentration, carrier compatibility, dispersion quality, and thermal resistance. A vivid sample can still fail beside a production line operating at 220°C.
A dependable buying process should examine seven practical areas. These include polymer compatibility, color measurement, dosage efficiency, migration resistance, weathering performance, regulatory documentation, and supplier technical support. ISO 1833 and ISO 10526-related color practices can support more consistent evaluation, but laboratory results never replace production trials. That is where many purchasing plans become too optimistic.
Ask for a retained sample. Test it in your actual PE grade. Check the first molded part, not only the laboratory plaque. Review batch-to-batch ΔE values, carrier data, and processing recommendations. A cheaper product may create higher costs through purging, rejects, or unstable shade matching. No supplier can remove every risk. However, transparent data, repeatable testing, and experienced technical guidance can make the risk visible before it reaches the customer.
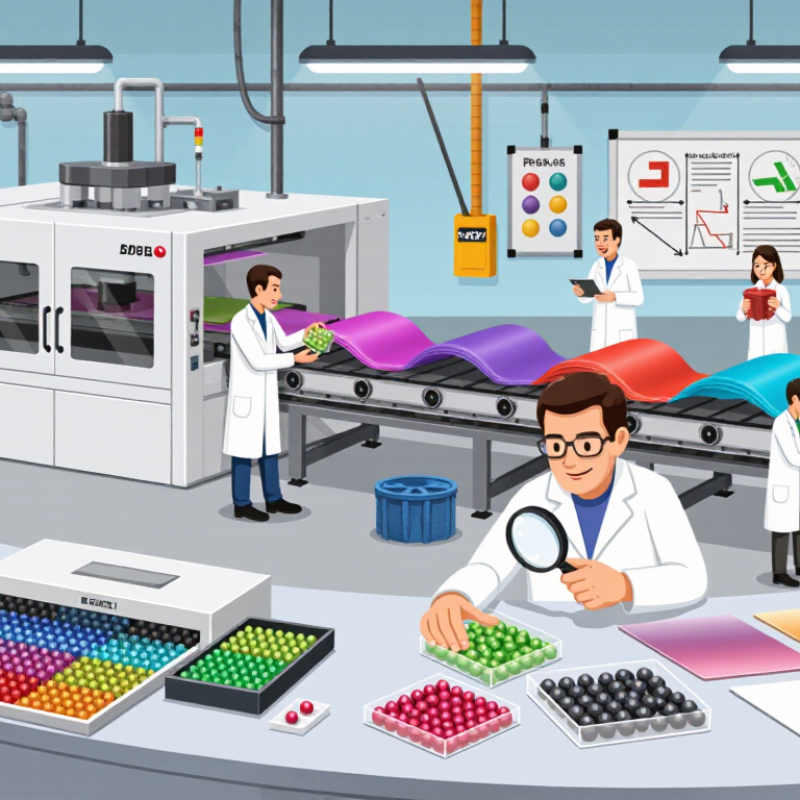
Table of Contents [Hide]
Understand PE Coloring Masterbatch and Its Main Applications
7 Tips for Buying PE Coloring Masterbatch?
Understand PE coloring masterbatch before comparing prices. It contains concentrated pigments, carrier resin, and processing additives. The carrier should match your polyethylene grade, such as LDPE, LLDPE, or HDPE. Poor compatibility may cause specks, streaks, weak welds, or uneven color. A bright sample can still perform poorly during production.
Tip 1: Define the application.
Film needs clean dispersion and low contamination. Injection-molded parts need heat stability and consistent shade. Blow-molded containers may require strong color uniformity across thin walls.
Tip 2:
Check the recommended let-down ratio.
Tip 3:
Request a technical data sheet and a physical sample. Compare both under your real processing temperature.
Color masterbatch supports packaging films, agricultural films, pipes, household containers, caps, toys, and industrial components. Each use has different demands. Outdoor products need suitable weather resistance. Food-contact applications require documented compliance for the target market.
Tip 4: Confirm pigment performance and regulatory documents.
Tip 5: Test migration, odor, and dispersion when relevant. These details are easy to overlook.
Tip 6:
Run a small trial using your actual resin and equipment. Record screw speed, temperature, dosage, and output appearance.
Tip 7:
Ask about batch consistency and storage conditions. Keep pellets dry, sealed, and away from direct heat.
A lower price may hide higher dosage or production waste. I would also question test results that lack method details. Color judgment is partly subjective, so use measured color data when possible.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.