o p t i m a r o b o t i c s
Blogs

7 Best Hot Extrusion Hydraulic Press Lines for Global Buyers

Choosing the right Hot Extrusion Hydraulic Press Line requires more than comparing tonnage and price. Global buyers must examine production goals, alloy types, billet dimensions, and local operating conditions. A press that performs well for aluminum profiles may struggle with copper, steel, or high-temperature alloys.

This guide reviews seven leading press lines through a practical purchasing lens. It considers extrusion force, container heating, ram stability, cycle time, energy use, and automated control. It also looks at billet loaders, cooling systems, die handling, and operator protection. These details shape daily output. They also affect maintenance costs.

Real factory experience matters.

Published specifications can look impressive, yet they may omit setup time or service limits. That gap deserves attention. Buyers should request test data, reference installations, spare-parts plans, and commissioning support before making a decision. Supplier experience with similar materials is equally important. Reliable manufacturers explain both strengths and limitations.

No single line fits every plant. Site power, foundation design, workforce skills, and regional service access can change the final choice. Some buyers may also underestimate training requirements. That is a common mistake. Careful comparison helps reduce that risk.

The following selection focuses on dependable engineering, measurable performance, and long-term value. It is designed to help procurement teams ask sharper questions and avoid decisions based only on catalog figures.
7 Best Hot Extrusion Hydraulic Press Lines for Global Buyers

How Hot Extrusion Hydraulic Press Lines Work

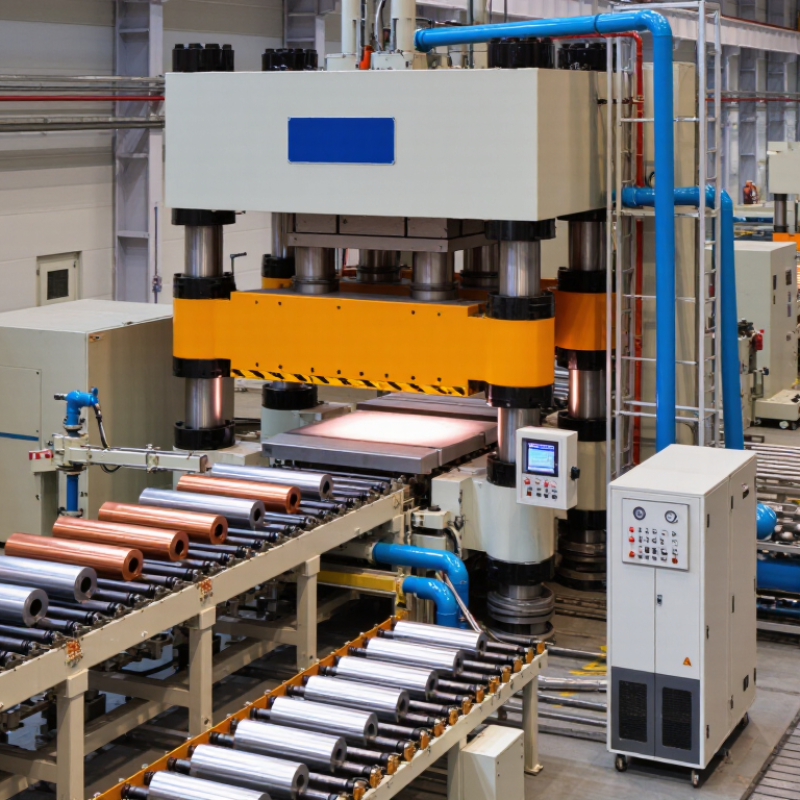
A hot extrusion hydraulic press line shapes heated metal through a die under controlled hydraulic force. The process begins when an induction furnace or gas furnace raises the billet to its working temperature. Aluminum may require a different range than copper or steel. Accurate temperature control matters because a cold billet increases forming resistance. An overheated billet can damage the surface or alter its structure.

A loader transfers the billet into the container, where the hydraulic ram pushes it forward. The metal flows through the die opening and emerges as a continuous profile. Pressure sensors monitor resistance during extrusion. Position sensors track ram movement with millimeter-level precision. Lubrication reduces friction between the billet, container, and tooling. Cooling equipment then stabilizes the profile before a puller moves it toward the cutting section.

The line also depends on alignment. Small errors can create uneven wall thickness, die wear, or surface tearing. Experienced technicians inspect the first profiles, adjust speed, and compare readings with previous production data. This part is less automatic than many brochures suggest. Heat loss between stations can change results unexpectedly. Operators may need to slow the ram or modify billet temperature. Maintenance teams check seals, hoses, valves, and die surfaces because hydraulic instability can quickly affect product quality. Clean records, calibrated instruments, and guarded moving parts support reliable operation for international buyers.

Seven Leading Hot Extrusion Hydraulic Press Line Configurations

Seven Leading Hot Extrusion Hydraulic Press Line Configurations

A hot extrusion line should match the alloy, billet size, profile geometry, and production rhythm. In practice, seven configurations appear most often: direct extrusion, reverse extrusion, vertical compact, horizontal high-tonnage, indirect profile, multi-station, and automated billet-to-cut lines. Each arrangement changes material flow, tooling access, and maintenance demands.

A direct extrusion line uses a heated billet, container, die, runout table, cooling section, and puller. It suits many standard profiles and offers familiar process control. Reverse extrusion reduces billet movement and can improve surface consistency for selected alloys.

A vertical compact line saves floor space, while a horizontal high-tonnage line handles larger billets and longer profiles. These choices need careful foundation planning. Vibration is easy to underestimate.

An indirect profile line can reduce friction and support difficult shapes, but its tooling system may require more specialized service skills. Multi-station lines combine heating, pressing, quenching, stretching, and cutting with limited manual handling. Automated billet-to-cut lines add sensors, transfer arms, recipe control, and guarded interfaces.

During commissioning, operators should verify billet temperature at several points, not only at the furnace display. Press speed, ram position, and die wear also need recorded checks.

No configuration is perfect. A compact line may restrict access during repairs, while a highly automated line can be difficult to troubleshoot without trained technicians. Proper guarding, interlocks, emergency stops, and documented maintenance remain essential for dependable operation.

Key Specifications for Comparing Press Line Performance

7 Best Hot Extrusion Hydraulic Press Lines for Global Buyers

Key Specifications for Comparing Press Line Performance

Comparing hot extrusion press lines requires more than checking nominal force. A 2,000-ton press may suit smaller aluminum profiles, while larger steel billets demand higher capacity. Review billet diameter, maximum billet length, container size, ram stroke, and extrusion speed together. These values reveal whether the line matches your planned products.

Cycle time is equally important. Check loading, pressing, return, cutting, and die-changing intervals. A fast ram cannot compensate for slow billet handling. Hydraulic pressure stability also affects surface quality and dimensional accuracy. Look for responsive pumps, pressure sensors, temperature monitoring, and rigid frame alignment. Energy use per billet provides a clearer operating-cost comparison than motor power alone. Higher power is not always higher productivity.

Tips: Request test data using your actual alloy, billet size, and die design. Ask for tolerance records, maintenance intervals, oil-filtration details, and emergency-stop response times. Inspect sample logs, not only brochure claims. A rated speed may be measured under ideal conditions. Real production is less perfect.

Control systems should record force, stroke position, oil temperature, and cycle history. This supports preventive maintenance and traceable quality checks.

Safety guarding, interlocks, and accessible service areas also deserve attention. I would leave room for uncertainty, because material behavior can change with heating accuracy and operator skill. A careful comparison includes trial results, spare-part access, installation support, and training requirements.

Material Compatibility and Industrial Applications

For global buyers comparing hot extrusion hydraulic press lines, material compatibility should lead the decision. Aluminum needs controlled billet heating, steady ram speed, and careful die cooling. Copper demands higher forming pressure and strong thermal management. Magnesium requires strict temperature control because its processing window is narrower. Steel extrusion can require greater force, tougher tooling, and reliable lubrication. A line sized only by maximum tonnage may still create weak profiles, surface tearing, or excessive scrap. Good selection links billet diameter, alloy behavior, die design, and press capacity.

These lines serve automotive structural parts, electrical conductors, window frames, heat sinks, and rail components. Construction favors repeatable aluminum profiles, while electrical production depends on clean copper surfaces and stable dimensions. Heavy engineering may use hot steel sections for demanding load conditions. During factory evaluations, buyers should inspect temperature uniformity, ram response, cycle records, and operator access. Ask for tested data with the intended alloy, not generic performance figures. That distinction matters. The first estimate is often optimistic. An overlooked detail is billet oxidation; it can damage surface quality before extrusion begins.

Tips: Match the press to the hardest planned alloy, then confirm tooling life. Request sample extrusions, defect data, and maintenance intervals. Leave capacity margin because real production is rarely perfect. Check local utilities, cooling systems, and worker training before installation. Small gaps here can become expensive delays.

Global Buyer Guide to Suppliers, Costs, and Compliance

7 Best Hot Extrusion Hydraulic Press Lines for Global Buyers

Global buyers should compare suppliers by proven production experience, not brochure speed alone. Request references for similar alloys, billet sizes, and annual output. A reliable supplier should provide drawings, load calculations, control documentation, and a clear acceptance procedure. Factory visits or live video inspections can reveal machining quality, wiring discipline, and maintenance access. Small details matter.

Quoted costs often exclude heating furnaces, dies, cooling systems, automation, installation, freight, customs duties, and operator training. Ask for a complete landed-cost estimate. Include spare seals, pumps, sensors, and critical electrical parts. These items may be expensive after shipment. Payment milestones should connect to design approval, factory testing, and final acceptance. I would not choose the lowest quote without checking its warranty response and delivery history.

Tips: Confirm material grades and output targets before requesting prices. Compare energy consumption, cycle time, and floor-space needs. Require a factory acceptance test using agreed samples. For compliance, verify applicable machinery-safety, electrical, pressure, and environmental requirements in the destination country. CE marking may apply in some markets, but it is not universal. Request risk assessments, manuals in the required language, conformity documents, and test records. Customs classification and import paperwork also deserve early review. A capable supplier should identify gaps, although buyers must obtain independent local advice. Naive assumptions create delays.

Brands

Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
Clients

Proudly Trusted by Top Companies Worldwide
Do you need Help? Get in touch.

X

Please fill out the form below and we will get back to you as soon as possible.

    Subscribe our newsletter & get updates