| Valve Design | Concentric, double-eccentric, or triple-eccentric butterfly valve design should be clearly identified, including the sealing mechanism and intended service conditions. | The design type, pressure class, temperature range, flow direction, and installation orientation are documented before quotation. | Approved drawings, sectional drawings, technical data sheets, and design calculation records. |
| Applicable Product Standard | The valve design and construction should follow a recognized butterfly valve standard suitable for the application. | Common references include EN 593, API 609, or another contractually specified equivalent standard. | Certificate of conformity, controlled product specification, and a clause-by-clause compliance statement. |
| Body and Disc Materials | Pressure-retaining and wetted materials must match the fluid, temperature, pressure, and corrosion conditions. | Material grades are stated on drawings and purchase documents; heat numbers are traceable to mill certificates. | Material test certificates, positive material identification records where required, and heat-number traceability. |
| Seat Material Selection | Seat material must be compatible with the medium, operating temperature, pressure differential, and cycle frequency. | Soft seats may provide bubble-tight shutoff within their rated limits; metal-seated designs require application-specific leakage acceptance. | Seat material specification, temperature limits, chemical compatibility data, and approved material certificates. |
| Machining Accuracy | Disc, shaft, body bore, seat-retaining surfaces, and flange interfaces should be machined to controlled tolerances. | Critical dimensions and tolerances are defined on controlled drawings and checked with calibrated instruments. | In-process inspection reports, dimensional records, calibration certificates, and nonconformance reports. |
| Pressure Boundary Test | The valve body and pressure-retaining components should be hydrostatically tested for structural integrity. | Testing is performed according to the purchase specification and a recognized test standard such as API 598 or ISO 5208. | Valve-specific pressure test report showing test medium, pressure, duration, temperature, gauge identification, and result. |
| Seat Leakage Test | The closed valve should be tested in the specified flow direction or both directions when required by the design and contract. | Acceptance is defined by the selected leakage class or rate in ISO 5208, EN 12266-1, API 598, or the project specification. | Recorded leakage rate, test pressure, stabilization time, test direction, seat condition, and authorized inspector signature. |
| Zero-Leakage Claim | “Zero leakage” should be treated as a defined test result rather than an unlimited operating guarantee. | The supplier states the applicable test standard, leakage class, pressure range, temperature, medium, and test duration. | Written leakage definition, witnessed test record, and contractually agreed acceptance criteria. |
| Operating Torque | Breakaway, running, and seating torque should be measured or calculated for the complete valve assembly. | Actuator sizing includes maximum differential pressure, seat friction, safety factor, and service temperature. | Torque calculation, test curve, actuator sizing sheet, and manual or automated operation record. |
| Shaft and Anti-Blowout Construction | The shaft connection and retention system should prevent unintended shaft displacement during operation or maintenance. | The design includes documented shaft retention and, where applicable, anti-blowout features. | Assembly drawing, design-risk review, inspection checklist, and functional operating test. |
| Flange and Face-to-Face Dimensions | Connection dimensions must match the piping system and the specified valve dimensional standard. | Face-to-face dimensions and flange drilling comply with the applicable standard or approved project drawing. | Dimensional inspection report, calibrated measuring equipment record, and final drawing approval. |
| Surface Protection | External coating, internal lining, or corrosion protection should be suitable for storage, transport, and service exposure. | Coating system, surface preparation, dry-film thickness, curing conditions, and repair procedure are specified. | Coating inspection report, dry-film thickness readings, surface-preparation record, and coating batch information. |
| Assembly Cleanliness | Valve internals should be free from machining chips, abrasive residue, welding debris, grease contamination, and foreign matter. | Cleaning and preservation procedures are defined according to the service, especially for oxygen, potable water, or hygienic applications. | Cleaning checklist, visual inspection record, preservation statement, and packing inspection photographs. |
| Actuator and Accessory Compatibility | Manual gearboxes, pneumatic actuators, electric actuators, limit switches, solenoid valves, and positioners must match the valve interface and torque requirement. | Valve mounting dimensions comply with ISO 5211 where applicable, and the complete assembly is function-tested. | Interface drawing, actuator data sheet, open-close cycle test, switch-setting record, and fail-position confirmation. |
| Production Traceability | Each valve should be traceable from raw material through machining, assembly, testing, marking, and shipment. | A unique serial number links the valve to material certificates, inspection records, test results, and final release documents. | Manufacturing record book, serial-number register, heat-number log, and final data-book index. |
| Quality Management System | The manufacturing facility should operate a documented quality management system with controlled procedures and corrective actions. | A current ISO 9001 certificate is verified against the issuing certification body and the actual manufacturing site. | Valid certificate, certification scope, latest surveillance status, internal audit records, and corrective-action samples. |
| Calibration Control | Pressure gauges, torque meters, dimensional tools, coating gauges, and electrical test instruments must be calibrated. | Calibration is current, traceable to recognized national or international measurement standards, and suitable for the required accuracy. | Calibration certificates, instrument register, due-date labels, and out-of-tolerance handling procedure. |
| Third-Party Inspection | Independent inspection may be used for material review, dimensional checks, pressure testing, coating inspection, and final release. | Inspection and Test Plans define hold points, witness points, document review, and rejection criteria before production begins. | Approved ITP, inspector qualifications, signed inspection reports, and release certificate. |
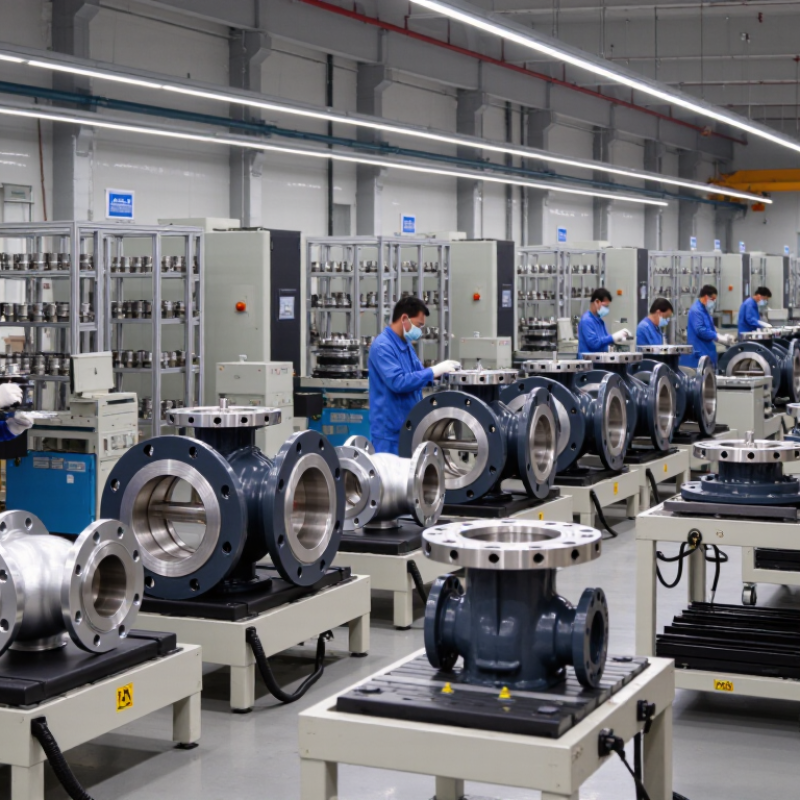
| Supplier Factory Audit | The buyer should verify manufacturing capacity, subcontractor control, testing facilities, warehouse conditions, and document management. | The audit covers actual production capability rather than only trading or office operations. | Audit checklist, production-line photographs, equipment list, employee competency records, and closed audit findings. |
| Sample Validation | Pre-production or production samples should be inspected and tested against the approved specification before volume shipment. | Sample approval includes dimensions, materials, operation, pressure boundary integrity, seat leakage, coating, and marking. | Approved sample report, signed inspection checklist, test certificates, and comparison against the purchase order. |
| Final Documentation | The final document package should be complete, consistent, and linked to each valve serial number. | The package includes drawings, material certificates, pressure and leakage test reports, inspection records, certificates, and operating instructions. | Indexed manufacturing data book, document-review checklist, and buyer-approved final release package. |
| Warranty and After-Sales Support | The supplier should define warranty coverage, exclusions, spare-parts availability, technical response time, and claim investigation procedures. | Warranty terms are written into the contract and supported by identifiable service contacts and replacement-part data. | Warranty certificate, spare-parts list, maintenance instructions, response procedure, and previous corrective-action examples. |