o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose the Right Square Tube for Global Sourcing?
When purchasing steel for international projects, choosing the right Square Tube is rarely a simple size decision. A 50 x 50 millimeter profile may look identical across suppliers. Its wall thickness, corner radius, steel grade, and straightness can differ significantly. These differences affect welding, load performance, corrosion resistance, and installation time. Experienced buyers examine the application before comparing prices. A low quotation can become expensive after rework, delays, or failed inspections. Good sourcing begins with a clear technical question. What must this tube withstand?
This guide explains the practical factors behind a dependable sourcing decision. Buyers should define dimensions, tolerance, surface finish, length, and required steel standards. They should also confirm whether the Square Tube is hot-formed, cold-formed, galvanized, or painted. Mill test certificates provide useful evidence, but documents alone cannot prove production consistency. Reviewing samples, factory photos, inspection records, and packaging methods adds valuable context. A reliable supplier should explain manufacturing limits clearly, not simply promise every specification. That matters during cross-border communication.
Small details often reveal larger risks. Uneven bundles may indicate weak handling controls. Unprotected ends can suffer dents during ocean transport. Moisture trapped inside wrapped tubes may create early rust. These problems are easy to underestimate. I have seen technically correct orders become difficult because packaging requirements were discussed too late. No checklist is perfect. Specifications can still miss real site conditions, especially when drawings change. Buyers should keep room for verification, independent inspection, and honest technical discussion. The best choice balances performance, compliance, delivery reliability, and total cost rather than selecting the cheapest Square Tube available.
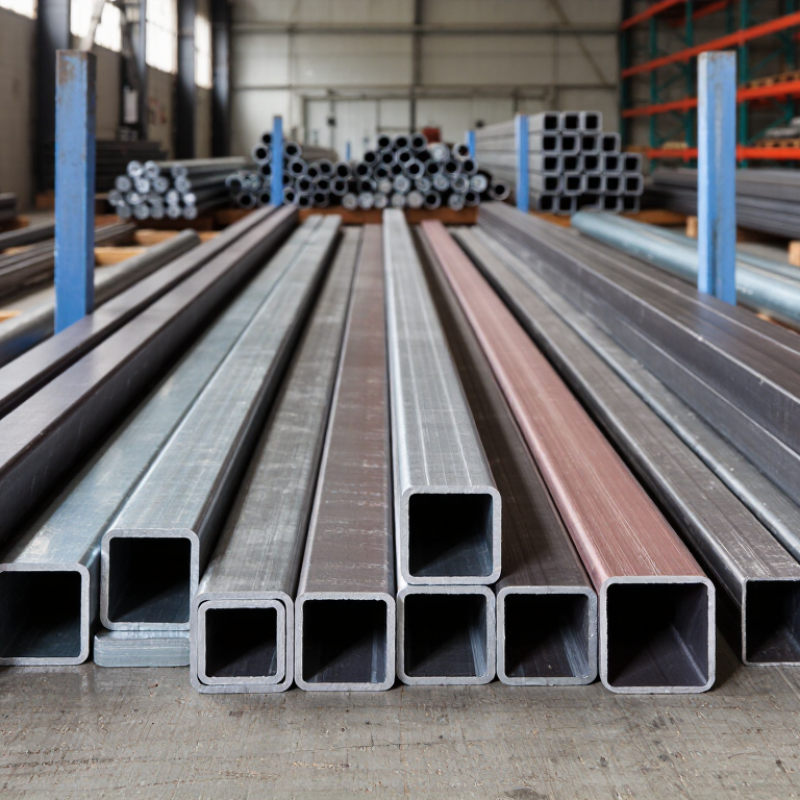
Table of Contents [Hide]
Define the Required Square Tube Application and Performance
Before choosing a square tube for global sourcing, define its exact job. A tube for a warehouse frame faces different demands than one used in furniture or machine guarding. Record the expected load, span, support method, and service temperature. Note whether the tube will be welded, bolted, painted, or left exposed. Small details matter.
For outdoor structures, review corrosion exposure, drainage, coating needs, and local humidity. For machinery, check dimensional accuracy, vibration, impact, and fatigue resistance. Wall thickness should match the load without creating unnecessary weight or transport cost. Confirm the steel grade, yield strength, tensile strength, and elongation through reliable test certificates. Ask for dimensional tolerances, corner radius, straightness, and surface condition.
Do not select by size alone.
A 40 × 40 mm tube can perform poorly if its wall is too thin or its corners are inconsistent. I have seen purchasing teams approve samples before testing weld behavior, then face cracking during production. That assumption can fail. Request production samples and inspect them under realistic conditions. Measure several points, not just one clean section. If the tube will be cut and joined locally, confirm compatible welding procedures and available equipment. Standards differ across markets, so compare the required specification with the destination project documents. A cheaper tube may create more rework, rejected assemblies, or delayed installation. Recheck the application when design conditions change.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.