o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose a Flame Laminating Machine
Choosing a Flame Laminating Machine requires more than comparing prices and production speeds. The right equipment must match your materials, daily output, workspace, and quality expectations. A machine suitable for mattress foam may perform poorly with automotive fabrics or coated textiles. Small differences matter.
Think about the production line in practical terms. What foam density will you process? How wide are your rolls? Will the material pass smoothly through the flame zone and nip rollers? Stable flame control, adjustable line speed, and consistent roller pressure directly affect bonding quality. A reliable cooling system also helps protect delicate fabrics after lamination.
Experience shows that impressive specifications do not guarantee good results. Some machines list high speeds but create uneven bonds at maximum output. That can lead to peeling edges, wrinkles, or wasted rolls. Slower production may be more efficient overall. Test samples using your actual foam, fabric, and adhesive requirements whenever possible.
Safety and service support deserve equal attention. Confirm that the supplier provides clear operating instructions, maintenance schedules, spare parts, and operator training. Check emergency stops, ventilation needs, flame monitoring, and access around heated components. These details support safer, more dependable production. Local technical support can prevent long delays when a sensor or roller needs attention.
A thoughtful buying decision should include total ownership cost. Consider energy use, replacement parts, cleaning time, labor, and expected downtime. Ask for documented performance data, not only promotional claims. There is no perfect machine for every factory. Careful testing remains the most honest guide.
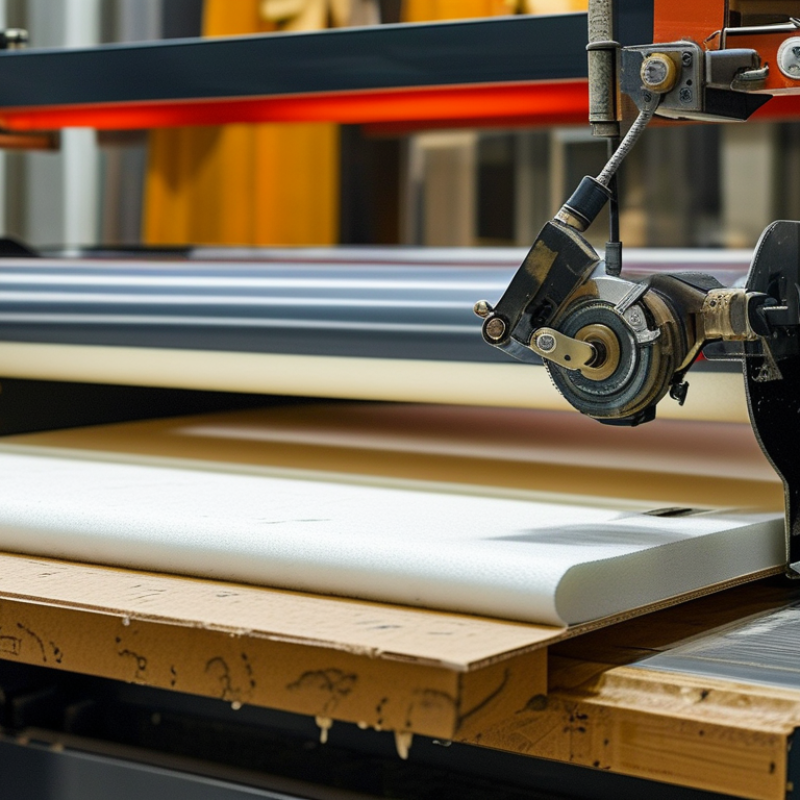
Table of Contents [Hide]
Define the Materials and Bonding Requirements
How to Choose a Flame Laminating Machine
Define the Materials and Bonding Requirements
When choosing a flame laminating machine, begin with the materials, not the machine’s advertised output. List every layer: foam, textile, film, coating, adhesive, and backing. Record thickness, width, density, moisture, and surface condition for each roll. Polyurethane foam may need a gentler flame than a dense rubber sheet. Some fabrics scorch quickly. Others resist bonding because their fibers carry finishes, oils, or dust. Ask for technical data sheets, but verify them with samples from actual production. Material names alone are not enough.
Define the bond before comparing machine specifications. Is the laminate required to resist peeling, washing, flexing, heat, or outdoor exposure? Set measurable targets for peel strength and acceptable appearance. Also define the bonding width, line speed, flame intensity, and temperature limits. During trials, inspect both sides after cooling. A bond that feels strong immediately may fail after aging. I once approved a sample too quickly, then found edge lifting after repeated bending. That mistake taught me to test under real stress. Not every successful trial deserves immediate approval.
Choose a machine with adjustment range, stable flame control, and clear monitoring. An operator should adjust treatment without guessing. Use controlled trials with fixed settings, then change one variable at a time. Keep records of roll batch, flame distance, speed, and test results. Ventilation, guarding, and trained operation are essential for reliable production. Do not chase speed first. A slower process may protect delicate materials and reduce rejects. If the material changes, repeat the validation. Small differences can matter.
How to Choose a Flame Laminating Machine - Define the Materials and Bonding Requirements
| Material or Requirement | Typical Material Structure | Key Properties to Confirm | Recommended Machine Considerations | Typical Starting Parameters | Quality Checks |
|---|---|---|---|---|---|
| Flexible polyurethane foam | Polyether or polyester PU foam bonded to textile, film, mesh, or nonwoven layers. | Density, thickness, cell structure, surface smoothness, flame response, compression recovery, and heat sensitivity. | Use a controlled flame zone, stable foam feeding, adjustable nip pressure, and web-tension control. The burner should provide an even flame across the working width. | Foam thickness: 2–30 mm Line speed: 5–30 m/min Begin with low-to-moderate exposure and increase gradually. | Check peel strength, foam shrinkage, surface scorching, bond uniformity, and whether the foam remains flexible after lamination. |
| Textile and fabric laminates | Knitted, woven, or nonwoven fabric laminated to foam, film, foil, or another textile. | Fiber type, fabric weight, stretch direction, porosity, coating or finishing, dimensional stability, and required hand feel. | Select a machine with accurate fabric alignment, low-tension unwinding, edge guiding, and sufficient cooling after the nip. | Fabric width: machine working width minus safety margin Bonding pressure: adjustable to prevent embossing Use lower tension for elastic or knitted fabrics. | Inspect for wrinkles, puckering, edge lift, adhesive-free areas, pattern distortion, and loss of stretch or drape. |
| Polyester or nylon fabrics | Synthetic textile bonded to PU foam, another fabric, or a thermoplastic film. | Melting or softening behavior, dye stability, coating compatibility, heat-shrinkage tendency, and required final strength. | Provide precise flame and speed adjustment. Include cooling or stabilization zones when the fabric is sensitive to heat distortion. | Common fabric weight: 40–300 g/m² Line speed: 8–35 m/min Use the lowest flame exposure that achieves continuous bonding. | Test color change, shrinkage, peel strength, abrasion resistance, wash durability, and bond appearance under transmitted light. |
| Polyolefin films and sheets | Polyethylene or polypropylene film, sheet, or coated textile combined with foam or fabric. | Low surface energy, film thickness, corona or plasma treatment, puncture resistance, shrinkage, and compatibility with the partner layer. | Confirm whether surface treatment is required. Use accurate web tracking, controlled nip pressure, and a process window that avoids film distortion. | Film thickness: approximately 20–500 μm Surface energy: verify by dyne testing Keep film tension low enough to prevent stretching. | Check delamination, bubbling, pinholes, wrinkles, film shrinkage, and bond strength after aging or flexing. |
| Foil, coated fabric, or barrier layer | Aluminum foil, metallized film, coated textile, or moisture-barrier layer laminated to a flexible substrate. | Coating adhesion, foil thickness, flex-crack resistance, barrier performance, surface cleanliness, and allowable heat exposure. | Choose a machine with smooth rollers, accurate alignment, low web tension, and gentle handling to avoid creasing or cracking the barrier layer. | Use moderate nip pressure Avoid direct overheating of the barrier layer Set speed according to the most heat-sensitive component. | Examine pinholes, cracks, wrinkles, barrier loss, peel strength, and visual uniformity after repeated bending. |
| Bond strength requirement | Permanent flexible bond between two continuous web materials. | Required peel strength, shear resistance, flexibility, fatigue life, wash or solvent resistance, and intended service temperature. | Select a machine capable of maintaining stable flame intensity, nip pressure, line speed, and web tension throughout the production run. | Define the target before machine selection Use laboratory trials to establish the speed–flame–pressure window rather than relying on one fixed setting. | Use a suitable 180-degree or 90-degree peel test method, record failure mode, and compare results before and after conditioning. |
| Production width and output | Single-width or multi-width roll-to-roll production. | Usable material width, roll diameter, core size, roll weight, daily output, changeover frequency, and available floor space. | Match the working width to the widest product, while allowing edge clearance. Consider automatic unwinding, rewinding, edge guiding, and recipe storage for repeatability. | Working width: product width plus edge allowance Speed range: select according to material trials Include acceleration and deceleration control for sensitive webs. | Verify actual output, roll hardness, telescoping, edge alignment, splice handling, and downtime during roll changes. |
| Safety and process control | Gas-fired open-flame process used with combustible polymeric materials. | Gas type and pressure, exhaust requirements, flame detection, emergency shutoff, operator access, and local regulatory requirements. | Require flame-failure protection, emergency stop circuits, guarded hot zones, adequate ventilation, gas-pressure monitoring, and accessible maintenance points. | Install according to local codes Use trained operators and documented startup, shutdown, and fault-reset procedures. | Inspect flame stability, exhaust performance, interlocks, emergency stops, gas connections, and combustible-residue buildup at scheduled intervals. |
| Trial and validation plan | Representative production materials from the intended product range. | Material batch variation, moisture content, surface contamination, storage history, and expected end-use conditions. | Request a material trial using actual production rolls. The machine should allow adjustment of flame intensity, line speed, nip pressure, and tension independently. | Test at low, nominal, and high speeds Record settings, material lot, ambient conditions, and test results for each trial. | Confirm bond strength, appearance, flexibility, dimensional stability, aging performance, and repeatability across multiple rolls. |
Selection principle: Final operating parameters must be established through controlled trials because foam formulation, fabric construction, surface treatment, thickness, moisture, and machine design can significantly change the bonding window.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.