o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose UHP Graphite Electrodes in 2026?
Choosing an UHP Graphite Electrode in 2026 requires more than comparing prices per ton. Steelmakers face stricter energy targets, unstable raw material costs, and higher expectations for furnace productivity. The correct electrode must match furnace power, transformer capacity, operating current, and tapping practice. A small mismatch can cause excessive oxidation, nipple damage, or unexpected breakage.
Experience matters here. Buyers should examine needle coke quality, bulk density, electrical resistivity, flexural strength, and thermal expansion. These figures should come from reliable test reports, not only a supplier’s product brochure. Pay close attention to electrode diameter, nipple design, machining accuracy, and the manufacturer’s quality controls. A detailed traceability system can reveal where each batch was produced and tested. Ask for recent performance data from furnaces with similar operating conditions.
UHP Graphite Electrode selection also involves practical supply decisions. Delivery stability, emergency stock, packaging quality, and technical support may influence production more than a low initial quotation. Inspectors should check threads, sealing surfaces, and visible cracks before installation. The process is not perfect. Laboratory values cannot fully predict every furnace event, and experienced operators may still disagree about the ideal grade. That uncertainty deserves honest discussion. A dependable supplier should explain limitations, provide corrective guidance, and support field verification. In 2026, the strongest choice will balance measurable performance, verified experience, lifecycle cost, and responsible purchasing. Performance first. Claims need evidence.
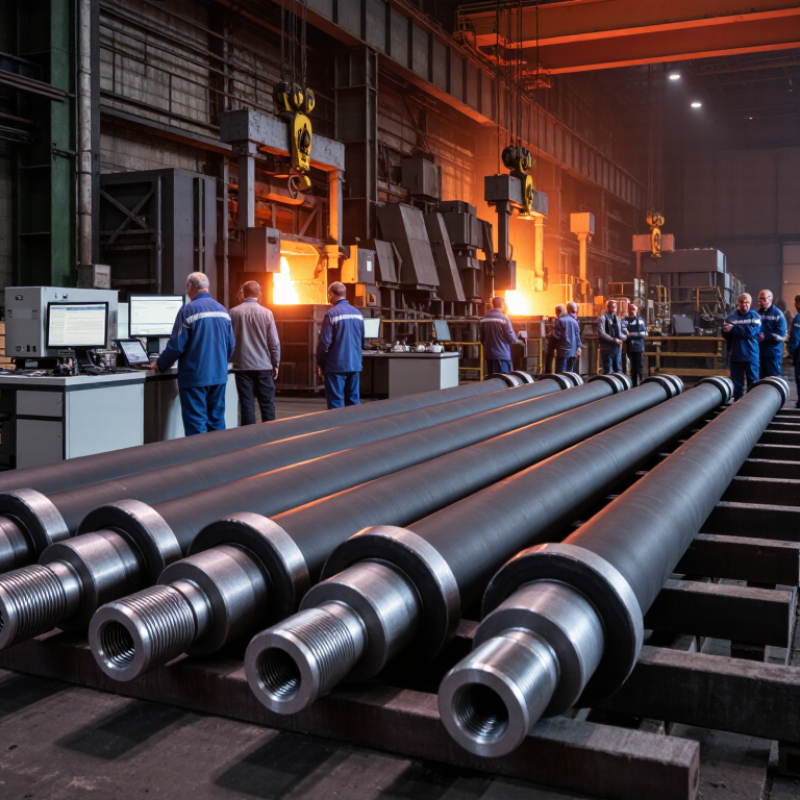
Table of Contents [Hide]
Understanding UHP Graphite Electrodes and Their Role in Steelmaking
How to Choose UHP Graphite Electrodes in 2026?
UHP graphite electrodes conduct extreme electrical current into electric arc furnaces. They withstand heat, mechanical stress, and repeated thermal shocks. Their role is central to scrap-based steelmaking.
The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023. Electric arc furnaces produced about 29% of that total. This share keeps electrode reliability commercially important.
UHP grades usually support current densities above 25 A/cm², according to common industry technical classifications. Higher current can shorten melting cycles and increase furnace productivity.
However, current density alone cannot determine electrode quality. Buyers should examine bulk density, electrical resistivity, flexural strength, oxidation resistance, and nipple performance.
A 600 mm electrode may appear suitable, yet poor joint precision can cause costly breakage during charging.
Look closely.
In 2026, selection should match furnace transformer capacity, operating current, steel grade, and tap-to-tap targets. The International Energy Agency identifies electric steelmaking as an important route for lowering emissions when electricity becomes cleaner.
That advantage weakens when electrodes oxidize rapidly or break unexpectedly. Practical users should request batch-level test certificates and review historical consumption per tonne of steel.
A common purchasing mistake is choosing the lowest price per tonne. The cheaper electrode may create longer outages, unstable arcs, and more carbon consumption.
No single specification works everywhere. Furnace data must decide.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.