o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose the Best Chamfering Cutter Supplier in China?
Choosing the best Chamfering Cutter supplier in China requires more than comparing online prices. The decision affects edge quality, tool life, production speed, and the consistency of finished parts. In daily machining, a cutter may appear acceptable while leaving uneven edges or visible burrs after repeated use. Small errors can increase rework and waste valuable material. The right supplier should understand these practical risks. Yet price alone remains a common buying factor. That assumption deserves careful review.
A reliable evaluation begins with technical evidence. Ask about carbide grade, cutter geometry, coating options, dimensional tolerance, and compatible materials. Request inspection reports and sample specifications before placing a large order. Check whether the supplier controls runout, cutting-edge sharpness, and surface finish during production. Photos are useful, but physical samples provide stronger evidence. Testing several pieces on your own equipment can reveal vibration, heat buildup, and actual tool durability. This step connects supplier claims with manufacturing experience. Do not skip it.
Supplier communication also reveals professional reliability. Clear answers about lead times, packaging, replacements, and quality procedures indicate stronger internal control. A trustworthy company should explain limitations instead of promising perfect results. Still, no supplier is perfect. Some catalogs may contain outdated data, and even experienced buyers can overlook application details. A trial order can expose these weaknesses early. Keep records of test results, feedback, and repeat performance. This guide will examine how to compare Chinese suppliers, verify their expertise, and select a Chamfering Cutter partner that supports stable, measurable production.
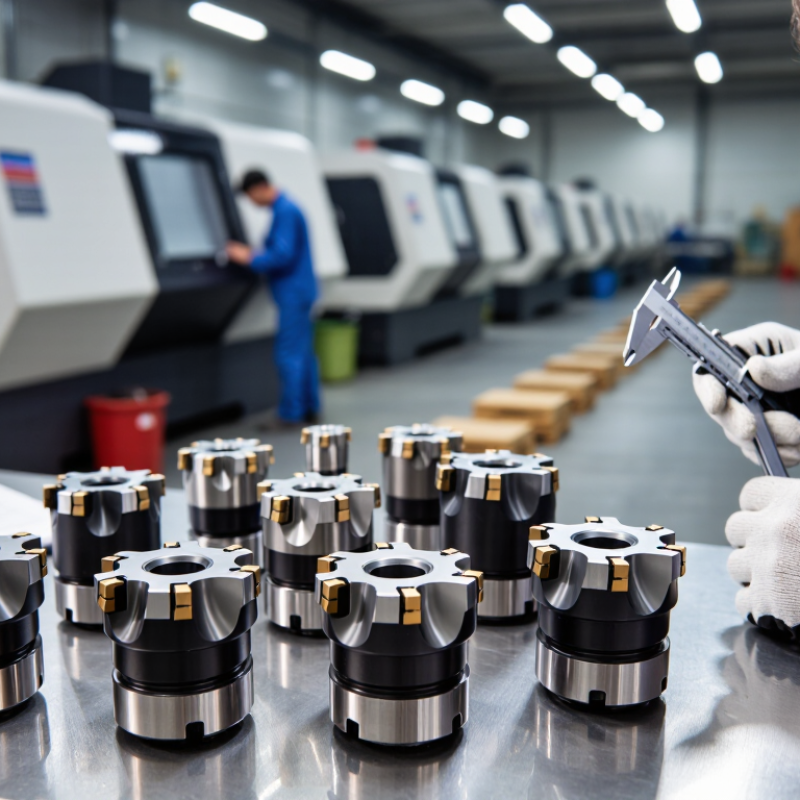
Table of Contents [Hide]
What Is a Chamfering Cutter and Why Does Supplier Selection Matter?
A chamfering cutter removes sharp edges and creates a clean angled surface on a workpiece. It may also prepare holes for screws, improve assembly, and reduce edge damage. Common types include countersink, carbide, and indexable cutters. Each design suits different materials, speeds, and production volumes.
Supplier selection matters because cutter quality affects accuracy, tool life, and surface finish. A reliable supplier should explain cutting geometry, coating options, tolerance limits, and recommended parameters. Ask for material certificates, inspection reports, and sample testing. A practical supplier will discuss your machine, workpiece material, and expected output instead of offering one universal solution. That detail shows technical experience.
Tips: Request a sample cutter before placing a large order. Check edge sharpness under good lighting. Measure the chamfer angle after machining. Review packaging, batch markings, and delivery records. Keep communication in writing. Small details matter.
Price still deserves attention. However, the cheapest cutter may create more rework and downtime. In my experience, supplier claims can sound precise but remain incomplete without test data. This is where careful comparison becomes important. Visit the factory online or in person when possible. Ask how workers inspect runout and edge geometry. A supplier that admits limitations may be more trustworthy than one promising perfect results every time. You should also confirm after-sales support, replacement policies, and response times before cooperation begins.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.