o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
Top PPGI Coated Coil Manufacturers and Suppliers
Choosing the right Ppgi Coated Coil manufacturer requires more than comparing prices. Buyers must examine coating quality, steel grade, production controls, and delivery reliability. A bright surface can hide weak adhesion. A low quote can also conceal inconsistent thickness.
This guide introduces leading PPGI coated coil manufacturers and suppliers across major producing regions. It considers their product ranges, coating systems, substrate options, certifications, and export experience. Practical details matter here. Buyers should check coil width, yield strength, paint type, coating mass, packaging, and test certificates. Traceability is equally important. Each coil should connect clearly to a production batch and inspection record.
Dr. Elena Markovic, a PPGI quality consultant, states, “A reliable coil begins with traceable steel, not a polished brochure.” Her observation reflects a common purchasing lesson. Supplier reputation helps, but documented performance matters more. Factory audits, sample testing, and verified references can reveal differences that catalogs often miss.
The market is not perfectly transparent. Some suppliers describe coating thickness differently. Others provide broad tolerances without explaining measurement methods. That creates avoidable uncertainty. Buyers may also overlook freight damage, storage humidity, and regional service support. These issues seem minor until rust appears around a cut edge.
The manufacturers discussed in this overview are evaluated through practical criteria. These include production capacity, technical support, quality consistency, customization, and communication. No supplier is ideal for every project. The best choice depends on climate, forming requirements, appearance standards, budget, and delivery schedule. A careful comparison can reduce rework and support longer-lasting building performance.
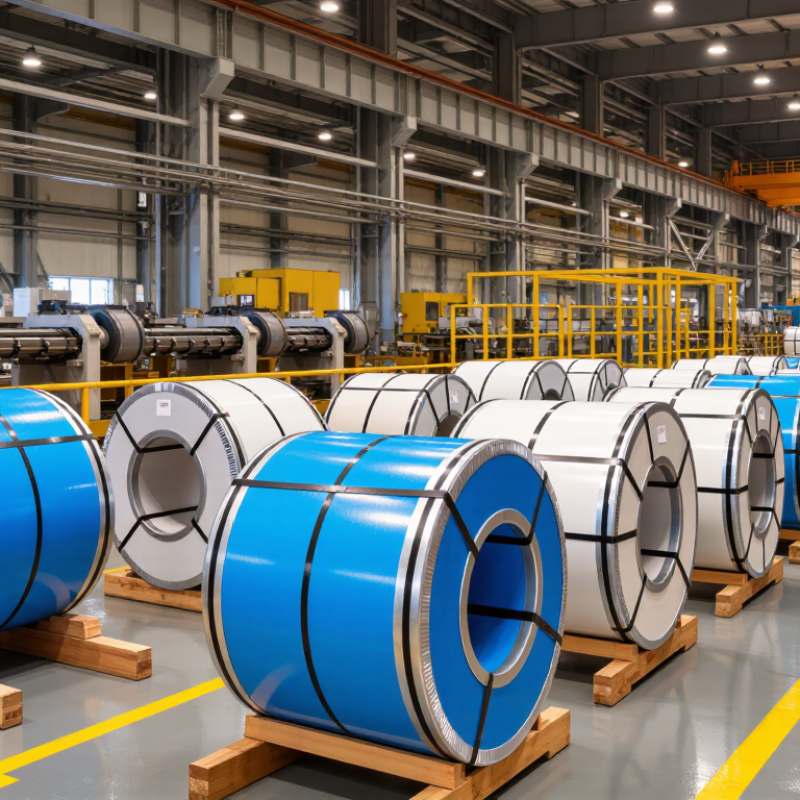
Table of Contents [Hide]
What PPGI Coated Coils Are and How They Are Made
PPGI coated coils are galvanized steel sheets painted before fabrication. The steel begins as a cold-rolled coil with a smooth, uniform surface. Manufacturers clean it carefully to remove oil, dust, and loose particles. Even a small residue can weaken paint adhesion.
The cleaned strip passes through a molten zinc bath. The zinc layer protects the steel from moisture and corrosion. After cooling, the surface receives chemical pretreatment, primer, and a colored topcoat. Rollers control the paint thickness across the moving strip. A curing oven then hardens each layer under carefully controlled heat.
In practice, the process is not flawless. Edge damage, uneven coating, or poor temperature control can appear during production. Quality teams inspect gloss, color, coating thickness, adhesion, and bending performance. They may also test samples after cutting or forming, because a coil can look perfect before fabrication.
A typical PPGI line runs continuously. Large recoilers then wind the finished strip into compact coils for transport and processing. Buyers should check the steel grade, zinc coating mass, paint system, thickness tolerance, and intended environment. Coastal air, industrial pollution, and frequent forming can require different specifications. Paint color matters, but the hidden layers matter more.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.