o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
7 Tips for Choosing the Right Metal Hole Saw
Choosing the right Metal Hole Saw can determine whether a drilling job ends cleanly or becomes a frustrating repair. A sharp, well-matched saw can cut through steel with steady pressure, while the wrong tool may overheat, chatter, or leave a jagged opening. Material thickness, hole diameter, and cutting speed all influence the result. Small details matter.
Experienced tradespeople usually inspect more than the advertised size. Bi-metal teeth suit many workshop tasks, while carbide-grit designs often handle tougher materials and abrasive surfaces. The arbor must match the drill and remain stable under load. A pilot drill also deserves attention, because excessive movement can damage the workpiece before the teeth engage. Manufacturer guidance remains essential, especially for stainless steel or thick plate.
Real working conditions can expose weaknesses that product descriptions overlook. A saw that performs well on a bench may struggle overhead or inside a cramped cabinet. Heat marks around the hole often signal excessive pressure, poor lubrication, or an unsuitable speed. Yet no selection guide is perfect; user technique, drill quality, and maintenance can change the outcome. These seven practical tips examine the choices that matter, from tooth design and diameter to cutting depth, compatibility, and service life. The goal is not simply to buy a larger or more expensive tool. It is to choose a Metal Hole Saw that matches the material, equipment, and actual demands of the job.
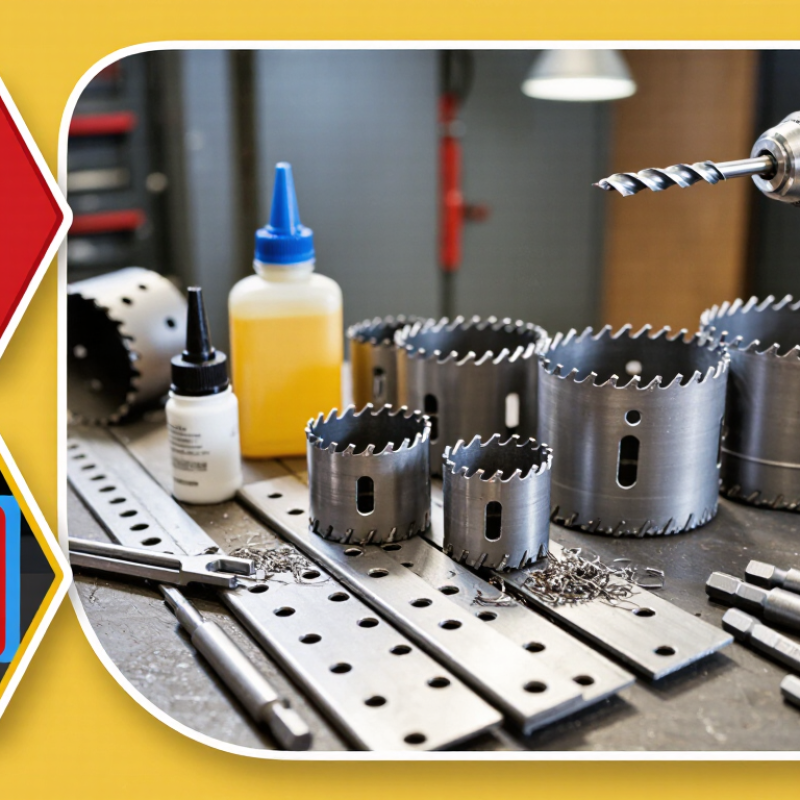
Table of Contents [Hide]
Classify the Workpiece: M35 HSS Has 5% Cobalt, While M42 Has 8%
Choosing the Right Metal Hole Saw
Classifying the workpiece is one of the most important decisions when selecting a metal hole saw. M35 high-speed steel contains about 5% cobalt, offering a practical balance of hardness, toughness, and cost. It suits mild steel, structural tubing, aluminum, and many general workshop applications. Keep the saw cutting steadily, not aggressively.
M42 contains about 8% cobalt. That extra cobalt improves hot hardness, helping the teeth resist softening when cutting stainless steel, tool steel, or other heat-resistant alloys. It is useful when friction builds quickly, especially in thick plate or repeated production work. However, a harder grade is not automatically better. A poorly selected tooth pitch or excessive cutting speed can damage either material.
I have seen good saws fail because the operator rushed the cut. Use firm pressure, suitable cutting fluid, and a speed matched to the workpiece diameter. Thin sheet may need finer teeth to prevent snagging, while thicker material often benefits from a variable pitch.
Check the chips: sharp, small curls usually indicate healthy cutting; blue chips suggest too much heat. M42 can tolerate more heat, but it cannot correct careless setup. I still reassess the choice when the workpiece contains welds, scale, or interrupted surfaces. Those details are easy to overlook.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.