o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
Why Choose a Ball Bearing CNC Machine?
Why Choose a Ball Bearing Cnc Machine?
A Ball Bearing Cnc Machine offers a practical balance between accuracy, speed, and repeatable production. Its spindle bearings support smooth rotation during drilling, milling, and precision boring. This matters when a bearing seat must remain round within tight tolerances. Even a small vibration can create chatter marks, heat, and costly scrap.
John Saunders, founder of Saunders Machine Works and a respected CNC educator, often shares a simple principle: “The best way to learn is by doing.” That idea applies directly to machine selection. Operators should inspect real test cuts, measure finished parts, and study performance under load. A polished brochure cannot replace a steel component measured after machining.
The right Ball Bearing Cnc Machine can reduce setup time and improve surface consistency. It may also handle repeated production with less manual correction. Picture a workshop producing bearing housings every morning. Consistent spindle movement helps each bore match the previous one. That consistency builds trust with customers.
Still, the machine is not a miracle. Poor tooling, incorrect feeds, or weak maintenance can defeat excellent hardware. Bearings need proper lubrication, clean coolant, and scheduled inspection. This is where many buyers underestimate ownership.
A careful buyer should compare spindle runout, bearing type, rigidity, service support, and control features. Ask for measured results, not impressive claims. Sometimes, a simpler machine is wiser. High speed alone does not guarantee better parts.
This guide examines why a Ball Bearing Cnc Machine may suit demanding workshops. It also considers its limitations, operating costs, and learning curve. Reliable results come from both engineering and disciplined human practice.
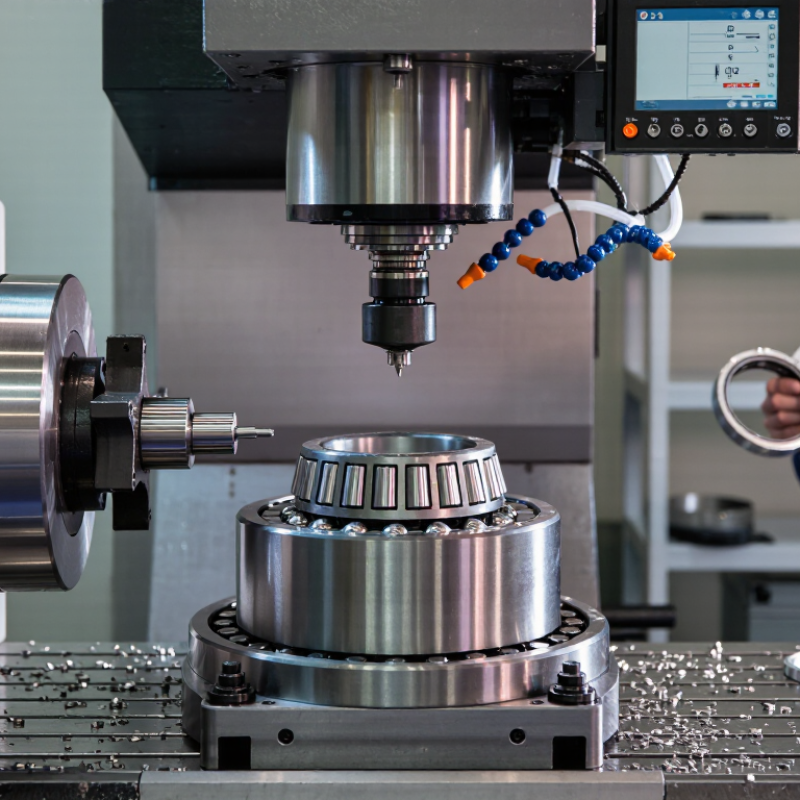
Table of Contents [Hide]
What Is a Ball-Bearing CNC Machine, and How Does It Work?
Why Choose a Ball Bearing CNC Machine?
A ball-bearing CNC machine uses hardened steel balls to support moving components with low rolling friction. In many designs, recirculating balls run inside linear guide blocks and ball screws. The screw converts motor rotation into controlled table movement. Preloaded bearings reduce play between mating surfaces. That matters when cutting small holes or repeating narrow contours.
The label can mislead. Not every bearing system delivers equal precision. Rail alignment, preload, lubrication, and machine stiffness also influence results. A practical check is simple: command a short axis move, then measure return position with a dial indicator. Heat, chips, and poor lubrication can still create errors. Small details matter.
According to Grand View Research, the global CNC machine market was valued at about 83.3 billion dollars in 2023. Its report links continued growth with automated, high-precision production. That demand explains the interest in low-friction motion systems. The U.S. Department of Energy reports that motor-driven equipment uses roughly 70% of industrial electricity. Efficient mechanical transmission can therefore support lower operating waste, although savings depend on the complete machine design.
Ball bearings also improve smoothness at moderate and high speeds. They can reduce vibration caused by uneven sliding contact. However, excessive preload increases friction and heat. More precision is not always better. A properly matched bearing system usually performs better than an aggressively tightened one.
Why Choose a Ball Bearing CNC Machine? - What Is a Ball-Bearing CNC Machine, and How Does It Work?
| System or Dimension | What It Is | How It Works | Typical Data or Range | Practical Benefit |
|---|---|---|---|---|
| Ball screw drive | A threaded shaft and nut containing recirculating steel balls. | The balls roll between the screw and nut, converting motor rotation into controlled linear movement with very low sliding friction. | Common lead: approximately 5–20 mm per revolution; many precision systems use preloaded nuts to reduce backlash. | Improves positioning consistency, efficiency, and repeatability compared with a basic sliding screw. |
| Linear ball-bearing guides | Guide blocks and rails that use recirculating balls to support and constrain an axis. | Rows of balls roll along hardened raceways while the guide block carries the table, gantry, or spindle assembly. | Typical rail sizes for compact machines: approximately 15–30 mm; larger machines may use larger rails and multiple blocks. | Provides smooth travel, high stiffness, and better resistance to side loads. |
| Drive motor and coupling | The motor-and-coupling assembly that rotates each ball screw. | A stepper or servo motor receives commands from the CNC controller and turns the screw by a calculated number of revolutions. | Typical positioning systems use stepper motors for lower-cost machines and servo motors where higher speed, feedback, and dynamic performance are required. | Controls axis speed and position while allowing coordinated multi-axis movement. |
| Encoder feedback | A position sensor used mainly with closed-loop servo systems. | The encoder reports actual motor or axis position to the controller, which corrects detected position error. | Feedback resolution varies by encoder and control system; it should not be confused with guaranteed machine accuracy. | Helps detect following errors, missed motion, and load-related position deviations. |
| Work envelope | The usable X, Y, and Z travel available for a workpiece. | The controller coordinates linear-axis movement within the machine’s programmed travel limits. | Compact machines commonly provide roughly 300–600 mm of X travel, 200–400 mm of Y travel, and 100–250 mm of Z travel. | Defines the maximum practical part size and influences fixture and tooling choices. |
| Positioning accuracy | How closely an axis reaches a commanded coordinate. | Accuracy depends on screw lead error, thermal expansion, guide alignment, calibration, structural rigidity, and control resolution. | A general small-machine range is approximately ±0.02–0.10 mm; published values must be checked under defined test conditions. | Supports dimensional control when the machine is properly calibrated and operated. |
| Repeatability | The ability to return to the same position repeatedly. | Preloaded rolling elements reduce clearance, while the controller repeats the programmed motion path. | Typical advertised values for compact precision machines may be around ±0.01–0.05 mm, depending on test method and setup. | Useful for repeated batches, drilling patterns, engraving, and multi-operation machining. |
| Rapid traverse speed | The maximum programmed axis speed when the machine is not cutting. | The controller accelerates the motor while staying within limits imposed by screw lead, motor torque, guide load, and machine rigidity. | Compact ball-screw machines commonly operate at approximately 3–15 m/min in rapid motion. | Reduces non-cutting time while maintaining controlled axis movement. |
| Spindle speed | The rotational speed of the cutting tool or workholding spindle. | The CNC controller sets spindle revolutions per minute according to the tool, material, diameter, and programmed cutting conditions. | Light-duty machines often use approximately 6,000–24,000 rpm; suitable speed depends on the application. | Enables cutting of materials such as plastics, wood, aluminum, and selected steels when the machine is appropriately designed. |
| Backlash control | Measures and methods used to limit lost motion when an axis reverses direction. | Preloaded ball nuts, proper bearing support, accurate alignment, and controller compensation reduce reversal error. | Well-adjusted systems aim for very low backlash, but the actual value must be measured on the completed machine. | Improves circular interpolation, corner accuracy, hole location, and surface quality. |
| Lubrication requirement | Oil or grease applied to ball screws, guideways, and bearings. | Lubricant separates rolling surfaces, reduces wear, and helps protect raceways from contamination. | Maintenance intervals vary with duty cycle, contamination, lubricant type, and manufacturer instructions. | Extends component life and helps preserve smooth, accurate motion. |
| CNC control process | The electronic system that interprets programmed toolpaths. | G-code commands are converted into coordinated axis pulses or servo commands; interpolation synchronizes X, Y, Z, and other axes. | Common functions include feed-rate control, spindle-speed control, work offsets, tool compensation, and limit protection. | Automates repeatable machining operations and allows complex geometries to be produced consistently. |
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.