o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
Why Choose a High Visibility Vest Manufacturer Factory?
Choosing a High Visibility Vest Manufacturer Factory is not merely a pricing decision. It affects visibility, comfort, consistency, and worker confidence in demanding environments. A reliable factory understands how fluorescent fabric, reflective tape, stitching, closures, and garment fit work together under real conditions.
Hugh Hoagland, a recognized personal protective equipment specialist, often says, “The best PPE is the PPE that gets worn.” That principle matters. A vest can meet a specification yet remain unused if it feels stiff, overheats the wearer, or tears near the pockets. Experienced manufacturers test practical details, including tape adhesion, seam strength, color consistency, wash durability, and size accuracy. They should also explain how products align with relevant standards, such as ANSI/ISEA 107 or EN ISO 20471, where applicable.
The factory floor reveals more than a polished brochure. Ask to see fabric inspection, reflective-tape placement, needlework control, and final packing checks. Traceable batch records add confidence when large orders reach different work locations. Still, no supplier is perfect. Sampling can miss a weak seam, and production pressure can reduce attention to detail. That is why independent testing, clear specifications, and regular communication remain valuable. A capable High Visibility Vest Manufacturer Factory does not simply promise bright garments. It demonstrates repeatable quality, responds honestly to problems, and helps buyers choose protection suited to actual work conditions.
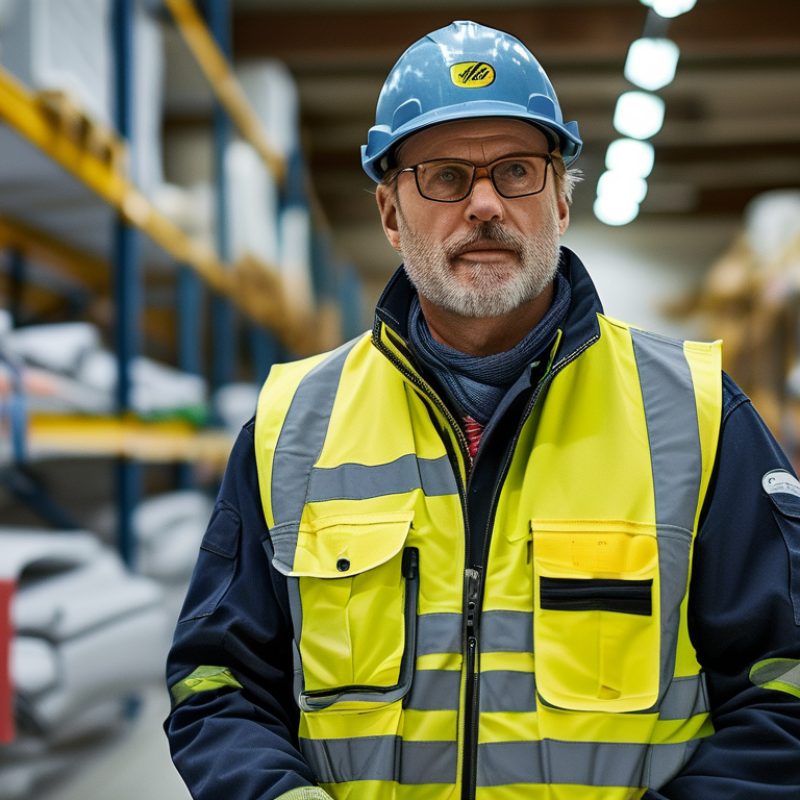
Table of Contents [Hide]
What Is a High Visibility Vest Manufacturer Factory?
A high visibility vest manufacturer factory is a production facility that designs, makes, tests, and controls reflective workwear. It is more than a trading office or online reseller. Its team selects fluorescent fabrics, reflective tape, thread, fasteners, and packaging. Workers then cut panels, sew seams, attach visibility materials, and inspect finished vests.
This process matters because small defects can reduce visibility. Poor stitching may open during movement. Incorrect tape placement can weaken a garment’s visual pattern. ANSI/ISEA 107-2020 defines performance classes for high visibility apparel, including background material and retroreflective elements. A capable factory uses these requirements during development, not only before shipment. The U.S. Bureau of Labor Statistics recorded 5,283 fatal work injuries in 2023. That figure does not prove that vests prevent incidents, but it shows why controlled safety equipment deserves careful attention. A factory cannot remove every workplace risk.
Tips: Ask for fabric specifications, test reports, sample inspections, and production photographs. Check whether the factory controls cutting and sewing internally. Confirm the vest’s intended work environment before choosing a performance class.
Experience also reveals uncomfortable details. A bright vest may look excellent under showroom lights but perform poorly after repeated washing. Reflective tape can crease. Sizing can fail across different body shapes. Reliable manufacturers record batch numbers, inspect high-risk seams, and review customer feedback. Still, no factory is perfect. A thoughtful supplier should admit limitations, explain testing methods, and improve weak points instead of promising flawless protection.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.